Copyright © 2025 Chuangming Coupling (Jiangsu) Co.,Ltd.
Assembly matters for the hot installation method of the jaw coupling
2026-09-23
During the hot assembly process, the heated component will cool down rapidly, which will affect the assembly quality. Therefore, preparations should be made before the assembly to minimize the assembly time. Before assembling the jaw coupling, the base plate of the reducer should be leveled, and heating and supporting pedestals should be welded on the base plate. The connection between the jaw coupling and the output shaft of the reducer has no tightening device. The torque is transmitted and the weight of the stirring paddle is borne by the assembly's clamping force.
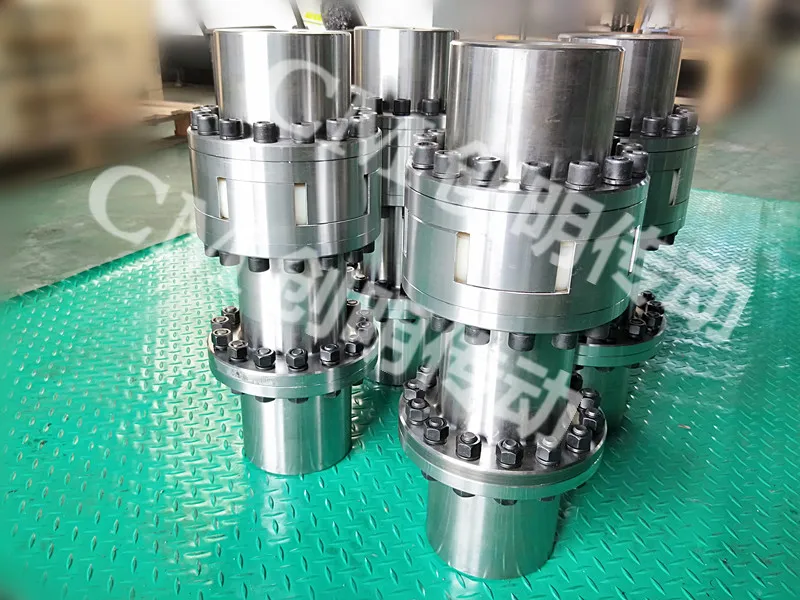
There should be a considerable interference fit between the shaft and the coupling. The assembly should be carried out using the hot mounting method. When assembling parts by hot assembly, the main principle is to utilize the property of objects' thermal expansion and contraction. After heating the accommodating part of the two parts that need to be assembled to a certain degree, they are immediately assembled onto the other component that fits them, reducing the interference fit or even creating a gap for assembly. Through contraction, the predetermined interference fit is achieved.
The hot mounting operation involves placing the component to be heated on a support platform, keeping it as far away from the shaft as possible. Start by using a heating torch to heat it, and continuously move the two heating torches to ensure uniform heating. Observe the the rmocouple instrument or use engine oil to test the temperature to avoid local overheating. Before reaching the heating temperature, continuously measure the hole diameter of the spline coupling with a template. Once the hole diameter template passes through, push the spline coupling to the bottom of the output shaft and align it with the assembly position for installation.
When lifting the jaw coupling, apply force evenly and continuously. If any deviation or jamming is found during the installation process, do not continue the operation. Correct the issue and reassemble. Once the jaw coupling reaches the shaft shoulder position, the assembly is completed. Remove the disassembly tools and slowly cool it down. During winter construction, corresponding protective measures should be taken. The cooling speed should not be too fast to prevent the jaw coupling from deforming or cracking.
During the hot assembly process, the heated component will cool down rapidly, which will affect the assembly quality. Therefore, preparations should be made before the assembly to minimize the assembly time. Before assembling the jaw coupling, the base plate of the reducer should be leveled, and heating and supporting pedestals should be welded on the base plate. The connection between the jaw coupling and the output shaft of the reducer has no tightening device. The torque is transmitted and the weight of the stirring paddle is borne by the assembly's clamping force.
There should be a considerable interference fit between the shaft and the coupling. The assembly should be carried out using the hot mounting method. When assembling parts by hot assembly, the main principle is to utilize the property of objects' thermal expansion and contraction. After heating the accommodating part of the two parts that need to be assembled to a certain degree, they are immediately assembled onto the other component that fits them, reducing the interference fit or even creating a gap for assembly. Through contraction, the predetermined interference fit is achieved.
The hot mounting operation involves placing the component to be heated on a support platform, keeping it as far away from the shaft as possible. Start by using a heating torch to heat it, and continuously move the two heating torches to ensure uniform heating. Observe the the rmocouple instrument or use engine oil to test the temperature to avoid local overheating. Before reaching the heating temperature, continuously measure the hole diameter of the spline coupling with a template. Once the hole diameter template passes through, push the spline coupling to the bottom of the output shaft and align it with the assembly position for installation.
When lifting the jaw coupling, apply force evenly and continuously. If any deviation or jamming is found during the installation process, do not continue the operation. Correct the issue and reassemble. Once the jaw coupling reaches the shaft shoulder position, the assembly is completed. Remove the disassembly tools and slowly cool it down. During winter construction, corresponding protective measures should be taken. The cooling speed should not be too fast to prevent the jaw coupling from deforming or cracking.
Previous: No more data